Vibro Shifter for Pharma Granulation Line – High Performance Powder Screening Solution
Introduction to Fluid Bed Dryer
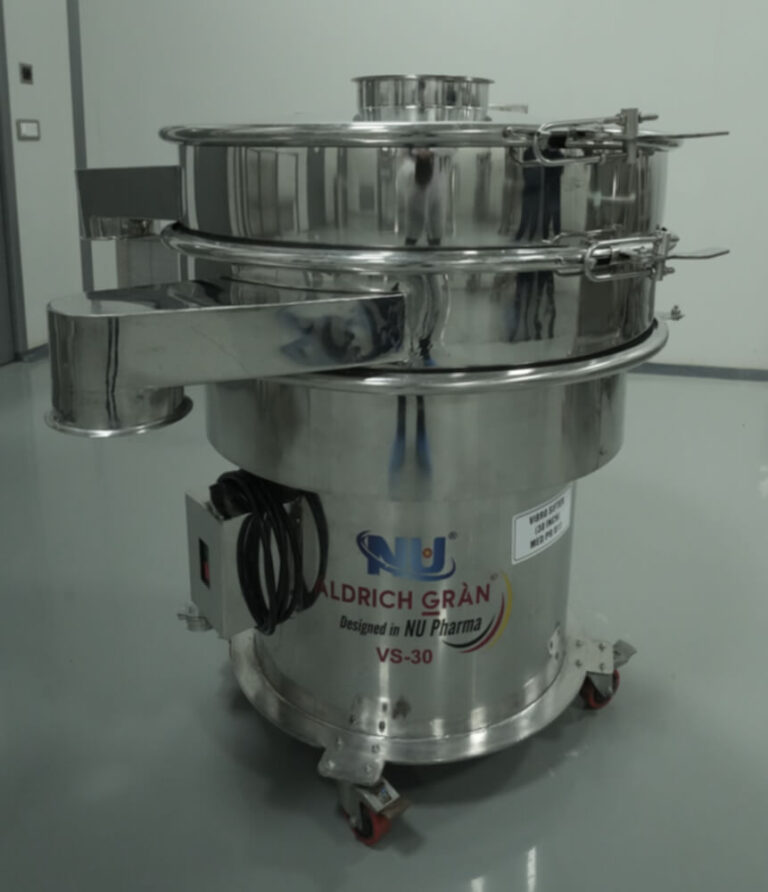
In pharmaceutical manufacturing, product quality depends on the consistency of every process. One of the most important stages in the granulation process is powder and granule screening. A Vibro Shifter for Pharma Granulation Line plays a critical role in ensuring uniform particle size, removing oversized particles, eliminating contaminants, and improving the overall quality of pharmaceutical products.
Whether manufacturing tablets, capsules, nutraceuticals, herbal medicines, or chemical powders, a pharmaceutical vibro shifter helps maintain GMP standards while increasing production efficiency.
At KNU PHARMA, we manufacture premium-quality Vibro Shifters engineered for modern pharmaceutical production lines. Our machines deliver high screening accuracy, hygienic construction, low maintenance, and reliable performance for continuous operation.
Share your requirements to our experts ? We are here for you
What is a Vibro Shifter?
A Vibro Shifter, also known as a Vibro Sifter, is a circular vibrating screening machine designed to separate powders and granules according to particle size.
The machine uses vibration generated by an unbalanced motor, allowing materials to move smoothly across the screening mesh. Oversized particles remain on the screen while fine particles pass through, resulting in consistent product quality.
The Vibro Shifter is widely used in:
- Pharmaceutical industries
- Nutraceutical manufacturing
- Chemical processing
- Food processing
- Cosmetic production
- Herbal medicine manufacturing
Importance of Vibro Shifter in Pharma Granulation Line
Granulation is one of the most important pharmaceutical manufacturing processes. After wet or dry granulation, the material contains particles of different sizes.
A Vibro Shifter helps by:
- Achieving uniform granule size
- Removing oversized particles
- Eliminating foreign contamination
- Improving tablet compression
- Enhancing capsule filling accuracy
- Increasing production efficiency
- Reducing material wastage
- Maintaining batch consistency
Without proper screening, tablets may experience weight variation, hardness issues, poor dissolution, and reduced product quality.
Working Principle of Vibro Shifter
The Vibro Shifter operates using a specially designed vibrating motor fitted with eccentric weights.
The vibration creates a three-dimensional movement that distributes the material evenly across the mesh screen.
The screening process involves:
- Material enters through the inlet.
- Vibrations spread the material uniformly.
- Fine particles pass through the mesh.
- Oversized granules remain above the screen.
- Separated material exits through dedicated outlets.
This continuous process ensures smooth operation with minimal product loss.
Features of Pharmaceutical Vibro Shifter
Modern Vibro Shifters offer several advanced features for pharmaceutical applications.
Stainless Steel Construction
Manufactured using SS304 or SS316 stainless steel for corrosion resistance and hygienic operation.
GMP Design
Smooth surfaces without dead corners ensure easy cleaning and compliance with pharmaceutical standards.
Low Noise Operation
Designed for quiet operation to improve workplace comfort.
High Screening Efficiency
Provides precise particle separation with high throughput.
Multiple Mesh Options
Different mesh sizes are available to suit various pharmaceutical products.
Dust-Free Operation
Enclosed design minimizes dust generation and improves workplace safety.
Easy Maintenance
Simple construction allows quick cleaning and reduced downtime.
Compact Design
Occupies less floor space while delivering high productivity.
Applications of Vibro Shifter in Pharmaceutical Industry
The Vibro Shifter is used in numerous pharmaceutical processes, including:
Tablet Manufacturing
Screens granules before compression for consistent tablet quality.
Capsule Manufacturing
Ensures uniform powder flow for accurate capsule filling.
API Processing
Separates active pharmaceutical ingredients according to required particle size.
Dry Powder Screening
Removes lumps and oversized particles.
Wet Granulation
Provides uniform granules before drying.
Nutraceutical Products
Screens vitamins, minerals, and protein powders.
Herbal Medicines
Separates herbal powders efficiently.
Cosmetic Powders
Used for talcum powder and cosmetic ingredients.
Benefits of Using Vibro Shifter
Installing a pharmaceutical Vibro Shifter provides several operational advantages.
Better Product Quality
Uniform particle size improves product consistency.
Higher Productivity
Continuous screening increases production capacity.
Reduced Rejection
Removes unwanted particles before further processing.
Improved Flowability
Uniform granules flow better during tablet compression.
Lower Maintenance Cost
Reliable construction minimizes maintenance.
Energy Efficient
Consumes less power while delivering high performance.
Hygienic Production
Closed design reduces contamination risk.
Long Equipment Life
Premium stainless steel ensures durability.
Technical Specifications
Typical specifications include:
- Material: SS304 / SS316
- Capacity: 50–2000 kg/hr
- Screen Diameter: 20″ to 72″
- Mesh Size: 10–500 Mesh
- Motor Power: 0.5 HP to 5 HP
- Voltage: 220V / 415V
- Frequency: 50 Hz
- Finish: Mirror Polish / Matt Finish
- GMP Compliance: Yes
- Dust Proof Design: Yes
Specifications may vary according to customer requirements.
Why Particle Size Matters in Pharmaceutical Manufacturing
Particle size directly influences:
- Tablet hardness
- Dissolution rate
- Drug absorption
- Uniform mixing
- Powder flow
- Compression quality
- Product stability
A Vibro Shifter ensures every batch maintains consistent particle distribution, improving manufacturing reliability.
Industries Served
Our Vibro Shifter machines are widely used in:
- Pharmaceutical Industry
- Nutraceutical Industry
- Food Processing
- Chemical Industry
- Cosmetics Industry
- Ayurvedic Medicine
- Veterinary Products
- Fine Chemicals
- Biotechnology
- Research Laboratories
Why Choose KNU PHARMA?
At KNU PHARMA, we focus on delivering reliable pharmaceutical processing equipment that meets international quality standards.
Our advantages include:
- GMP-compliant manufacturing
- Custom machine sizes
- Premium stainless steel construction
- High screening accuracy
- Competitive pricing
- Fast delivery
- Technical support
- Spare parts availability
- Low maintenance design
- Long operational life
Our experienced engineering team provides customized solutions based on your production capacity and application requirements.
Maintenance Tips
Regular maintenance improves machine performance and lifespan.
Recommended practices include:
- Clean the mesh after every batch.
- Inspect vibration motor regularly.
- Tighten fasteners periodically.
- Replace damaged mesh immediately.
- Lubricate bearings as recommended.
- Keep the machine dust-free.
- Perform preventive maintenance according to schedule.
Proper maintenance minimizes downtime and ensures consistent screening quality.
Safety Features
Modern Vibro Shifters include several safety features:
- Fully enclosed construction
- Food-grade contact parts
- Low vibration transmission
- Emergency stop option
- Stable base frame
- Secure clamping system
- Dust-proof sealing
- Easy cleaning design
These features support safe operation in pharmaceutical production environments.
Conclusion
A Vibro Shifter for Pharma Granulation Line is an essential machine for ensuring uniform particle size, superior product quality, and efficient pharmaceutical manufacturing. By removing oversized particles and improving powder consistency, it enhances tablet compression, capsule filling, and overall process reliability.
At [Your Company Name], we offer high-performance pharmaceutical Vibro Shifters built with GMP-compliant designs, premium stainless steel construction, and advanced vibration technology. Whether you need a standard model or a customized solution, our equipment is designed to improve productivity, reduce downtime, and meet the demanding requirements of the pharmaceutical industry.
For businesses seeking reliable powder screening solutions, investing in a high-quality Vibro Shifter is a smart step toward better product quality, regulatory compliance, and long-term operational efficiency.
What is a Vibro Shifter used for?
It is used to separate pharmaceutical powders and granules according to particle size while removing impurities.
What materials are used?
Most pharmaceutical Vibro Shifters are manufactured using SS304 or SS316 stainless steel.
Is the machine GMP compliant?
Yes. Pharmaceutical Vibro Shifters are designed according to GMP requirements.
Can different mesh sizes be installed?
Yes. Mesh screens can be changed based on product requirements.
Is it suitable for continuous operation?
Yes. Industrial Vibro Shifters are designed for continuous production.
What products can be screened?
Powders, granules, APIs, nutraceuticals, herbal powders, chemicals, and food ingredients.