Inline Homogenizer for Liquid Oral Syrup & Suspension Manufacturing Plant
Introduction
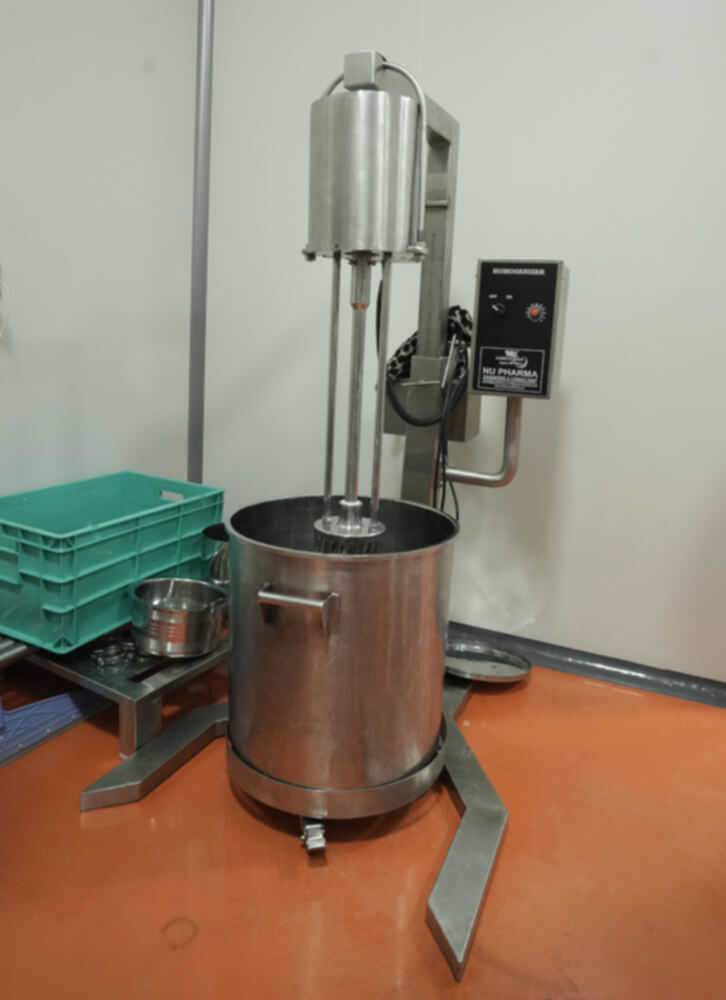
An Inline Homogenizer for Liquid Oral Syrup & Suspension Manufacturing Plant is an advanced pharmaceutical processing machine designed to achieve uniform mixing, particle size reduction, and stable dispersion of ingredients in liquid formulations. It plays a crucial role in the manufacturing of oral syrups, oral suspensions, emulsions, and other liquid pharmaceutical products where consistent quality and excellent product stability are required.
In pharmaceutical manufacturing, maintaining the correct viscosity, smooth texture, and uniform distribution of active pharmaceutical ingredients (API) is essential. A high-performance pharmaceutical inline homogenizer helps manufacturers achieve these requirements by providing efficient high-shear mixing and continuous homogenization.
Share your requirements to our experts ? We are here for you
What is an Inline Homogenizer?
An Inline Homogenizer is a high-speed mixing system installed directly into a processing pipeline or recirculation loop. Unlike traditional batch mixers, an inline homogenizer continuously processes the product as it flows through the system, creating intense shear forces that break down particles, eliminate lumps, and improve dispersion.
The machine consists of a rotor-stator assembly that generates high mechanical shear, allowing rapid mixing of liquid ingredients, powders, active ingredients, stabilizers, and other formulation components.
Importance of Inline Homogenizer in Liquid Oral Syrup Manufacturing
Liquid oral syrups require precise blending of active ingredients, sweeteners, flavors, preservatives, and other excipients. An inline homogenizer machine for syrup manufacturing ensures:
- Uniform distribution of active ingredients
- Smooth and consistent product texture
- Improved dissolution and dispersion
- Reduced processing time
- Enhanced product stability
- Better batch-to-batch consistency
The homogenization process helps prevent ingredient separation and ensures every dose contains the required concentration of medication.
Role of Inline Homogenizer in Oral Suspension Manufacturing
Oral suspensions contain insoluble drug particles that must remain evenly dispersed throughout the liquid medium. Poor mixing can lead to sedimentation, inconsistent dosing, and reduced product effectiveness.
A high shear inline homogenizer for pharmaceutical suspension manufacturing provides:
- Controlled particle size reduction
- Improved suspension stability
- Uniform API distribution
- Prevention of agglomeration
- Better flow characteristics
- Extended shelf life of formulations
This makes inline homogenization an important step in producing high-quality pharmaceutical suspensions.
Key Features of Pharmaceutical Inline Homogenizer
Modern inline homogenizers used in liquid pharmaceutical plants are designed with advanced features, including:
High-Shear Rotor-Stator Technology
The rotor-stator system creates powerful shear forces that efficiently break down particles and ensure complete mixing.
Continuous Processing Capability
Inline operation allows continuous circulation and processing, reducing manufacturing time compared with conventional batch mixing methods.
Hygienic Pharmaceutical Design
Equipment is manufactured using stainless steel construction, typically SS 316/316L contact parts, to meet pharmaceutical hygiene and cleaning requirements.
Easy Cleaning and Maintenance
Designed for pharmaceutical applications, inline homogenizers support easy dismantling, cleaning, and maintenance procedures.
Scalable Production
These systems are suitable for laboratory, pilot-scale, and large-scale pharmaceutical manufacturing plants.
Applications of Inline Homogenizer in Pharmaceutical Manufacturing
Inline homogenizers are widely used for manufacturing:
- Oral syrups
- Oral suspensions
- Emulsions
- Liquid nutraceutical formulations
- Herbal liquid products
- Cosmetic creams and lotions
- Pharmaceutical dispersions
Advantages of Using Inline Homogenizer in Syrup & Suspension Plants
Installing an inline homogenization system offers several benefits:
Improved Product Quality
The machine ensures consistent mixing and uniform formulation characteristics.
Faster Manufacturing Process
High-speed homogenization reduces processing time and increases production efficiency.
Better Stability of Formulations
Fine particle dispersion helps prevent separation and improves product shelf life.
Reduced Production Waste
Efficient mixing minimizes batch failures caused by poor dispersion or uneven formulation.
Enhanced Regulatory Compliance
Pharmaceutical-grade homogenizers support manufacturing processes that follow strict quality standards.
Inline Homogenizer vs Conventional Mixing System
| Feature | Inline Homogenizer | Conventional Mixer |
|---|---|---|
| Mixing Efficiency | High shear continuous mixing | Standard agitation |
| Particle Reduction | Excellent | Limited |
| Processing Time | Faster | Longer |
| Product Uniformity | High consistency | Variable |
| Suspension Stability | Improved | Moderate |
Choosing the Right Inline Homogenizer for Pharmaceutical Manufacturing
When selecting an inline homogenizer for a liquid oral syrup or suspension manufacturing plant, manufacturers should consider:
- Production capacity
- Product viscosity
- Required particle size
- Batch volume
- Material compatibility
- Cleaning requirements
- GMP compliance
- Automation requirements
A properly selected homogenization system improves production efficiency and ensures consistent pharmaceutical product quality.
Conclusion
An Inline Homogenizer for Liquid Oral Syrup & Suspension Manufacturing Plant is an essential piece of equipment for achieving reliable, stable, and high-quality pharmaceutical liquid formulations. With advanced rotor-stator technology, continuous processing capability, and efficient particle size reduction, inline homogenizers help manufacturers produce uniform oral syrups and suspensions that meet modern pharmaceutical industry standards.
Investing in a pharmaceutical-grade inline homogenizer improves productivity, enhances product stability, and supports the development of safe and effective liquid medicines.